Content Menu
● 1. 1. Understanding Wood Look Fiberglass Front Doors: Types and Applications
● 2. 2. Wood Look Fiberglass Front Doors Quality and Performance Factors
● 3. 3. How to Evaluate Wood Look Fiberglass Front Doors Suppliers
● 4. 4. Key Quality Indicators for Wood Look Fiberglass Front Doors Buyers
● 5. 5. The Middleman Problem and Direct Sourcing
● 6. 6. Our Manufacturing Capabilities
● 7. 7. Customization and OEM/ODM Options
● 8. 8. Ordering Process and Logistics
13 min read
When an overseas buyer places their first container order for wood look fiberglass front doors, the question they ask is rarely about price. It is about whether the factory can replicate the sample quality at scale. This concern is justified. The gap between a showroom prototype and a production run has sunk more procurement deals than any pricing dispute.
The entry door market has undergone a quiet revolution. Architects and contractors still specify the warm aesthetic of wood, but they increasingly write purchase orders for fiberglass. The reasons go beyond durability. This guide covers the technical specifications, procurement frameworks, and supply chain considerations for sourcing wood look fiberglass front doors in bulk.
1. Understanding Wood Look Fiberglass Front Doors: Types and Applications
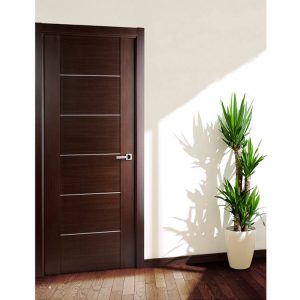
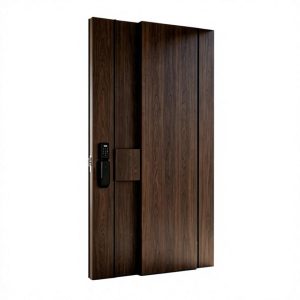
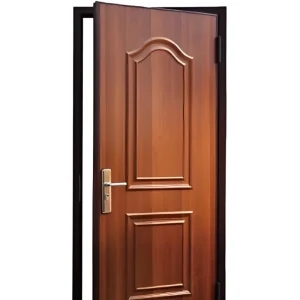
Wood look fiberglass front doors are exterior entry doors manufactured with a fiberglass reinforced polymer (FRP) skin that replicates the appearance of natural wood grain. The core typically consists of polyurethane foam insulation, and the frame is reinforced with composite or steel materials.
The product category serves three distinct markets. High-end residential villas use them for their aesthetic appeal and thermal performance. Commercial projects such as hotels and office buildings specify them for their dimensional stability and low maintenance. Coastal and desert regions favor them because they resist moisture, salt air, and extreme UV exposure without warping.
1.1 The Three Construction Types
Buyers encounter three construction methods, and the differences matter for performance and price.
| Construction Type | Skin Material | Core Material | Best Application | Relative Cost |
|---|---|---|---|---|
| Compression Molded | Fiberglass sheet molding compound (SMC) | Polyurethane foam | Residential, commercial | High |
| Resin Transfer Molded | Fiberglass with resin infusion | Polyurethane foam | Premium architectural | Highest |
| Hand Lay-Up | Fiberglass mat with resin | Foam or honeycomb | Budget projects | Low |
Compression molded doors dominate the market. The process involves pressing fiberglass sheets and resin between heated molds under high pressure. This creates a dense, impact-resistant skin with detailed wood grain texture. Resin transfer molding offers better surface quality but at a higher cost. Hand lay-up construction is cheaper but often shows defects like print-through, where glass fibers become visible under the paint after a few seasons.
1.2 Performance Metrics: Thermal Efficiency and Structural Integrity
The thermal performance data tells the story clearly. A solid wood door with no glazing delivers an R-value of approximately R-2 to R-3, translating to a U-factor around 0.35 to 0.50. An insulated fiberglass door with a polyurethane foam core typically achieves R-5 to R-7, with U-factors between 0.15 and 0.20 [1].
For a 20-square-foot door opening, the difference between a U-factor of 0.35 and 0.18 represents roughly 340 BTUs per hour in heat loss. Over a heating season in a northern climate, that adds up to significant energy savings.
Fiberglass also has a coefficient of thermal expansion that is approximately one-tenth that of wood. This means the door does not swell in summer humidity or shrink in winter dryness. For contractors, this translates directly into fewer service callbacks for sticking doors or failed weatherstripping.
1.3 Popular Wood Grain Finishes and Textures
The “wood look” is not a single aesthetic. Manufacturers offer several distinct grain patterns.
- Oak: A prominent, straight grain with moderate texture. The most common choice for traditional architecture.
- Mahogany: A tighter, more uniform grain with a reddish-brown undertone. Popular for luxury projects.
- Knotty Alder: A rustic appearance with pronounced knots and irregular grain. Frequently specified for mountain or lodge-style homes.
- Walnut: A dark, rich grain with subtle striping. Used in modern and transitional designs.
The finish quality depends on the mold texture and the coating system. A good embossed texture has visible pores and subtle depth that catches light. A poor one looks flat and painted. The best finishes use a multi-coat process: a base color, a glaze that sits in the embossed pores, and a clear topcoat for UV protection.
2. Wood Look Fiberglass Front Doors Quality and Performance Factors
Not all fiberglass doors perform equally. The material composition and manufacturing process determine whether a door lasts 20 years or fails within 5.
2.1 The Resin-to-Glass Ratio
Fiberglass strength comes from the glass fibers, not the resin. The resin binds the fibers and provides surface hardness. A door with insufficient glass content will flex under load and show print-through over time. Quality manufacturers use a glass content of 25-30% by weight in the skin. Budget manufacturers often drop this to 15-20% to save cost.
Buyers cannot verify this ratio from a sample alone. They must request the material data sheet or test certificate from the supplier.
2.2 Core Density and Thermal Performance
The polyurethane foam core determines the insulation value. Foam density varies from approximately 2 to 4 pounds per cubic foot. Higher density foam provides better insulation and more structural rigidity. Some manufacturers use a lower-density foam to cut costs, which reduces the R-value and makes the door feel hollow when closed.
One way to check core quality is the door weight. A standard 36-inch by 80-inch fiberglass door with a quality foam core weighs approximately 120 to 150 pounds. A door that weighs significantly less likely has a thinner or lower-density core.
2.3 The Frame and Edge Sealing
The door skin is only part of the system. The frame, typically made of composite or reinforced PVC, must be designed to prevent water intrusion. The edge sealing—where the skin meets the frame—is a common failure point. Poor sealing allows moisture to enter the core, causing delamination and swelling.
Manufacturers use one of two methods: a mechanical crimp that interlocks the skin and frame, or an adhesive bond. The mechanical crimp is generally more reliable for long-term durability.
2.4 Glass and Hardware Integration
Most wood look fiberglass front doors include glazing. The glass package significantly affects both thermal performance and security. Buyers should specify:
- Low-E coating: A microscopically thin metallic layer that reflects heat while transmitting light.
- Argon or krypton gas fill: Inert gas between double or triple panes that reduces heat transfer.
- Warm-edge spacers: Non-metallic spacers at the glass edge that reduce heat loss at the perimeter.
- Tempered or laminated glass: Tempered glass is required by code in many jurisdictions. Laminated glass offers additional security and sound reduction.
The hardware integration matters equally. A wood look fiberglass door should accept standard mortise locksets, multi-point locking systems, or smart locks. The manufacturer must machine the door skin and frame to accept these components during production, not as a field modification.
3. How to Evaluate Wood Look Fiberglass Front Doors Suppliers
The supplier selection process determines project success more than any other factor. A structured evaluation framework reduces risk.
3.1 Quality Control and Testing Standards
Buyers should ask for test reports that verify performance claims. The relevant standards for exterior doors include:
- ASTM E283: Air infiltration testing
- ASTM E547: Water penetration testing
- ASTM E330: Structural performance under wind load
- ASTM E1886 / E1996: Impact resistance for hurricane-prone regions
A reputable manufacturer conducts these tests on finished doors, not just component materials. The test report should show the specific model number and configuration tested.
3.2 The Inspection Checklist
Before placing a bulk order, buyers should verify the following:
- Surface quality: No visible print-through, bubbles, or uneven texture
- Dimensional accuracy: Width, height, and squareness within tolerances of ±1/16 inch
- Color consistency: No variation between doors in the same production run
- Hardware alignment: Hinges, locks, and handles align properly with no binding
- Weatherstripping: Seals compress evenly when the door closes
- Glass package: Low-E coating present, no visible defects in the glazing
3.3 Red Flags to Avoid
Several warning signs indicate a supplier may not deliver acceptable quality:
- No test data available: If a supplier cannot provide test reports, assume the product has not been tested.
- Vague material specifications: A supplier who cannot state the resin-to-glass ratio or foam density likely does not control their production process.
- Sample quality exceeds production quality: A common tactic is to hand-finish samples while producing lower-quality goods in volume.
- No pre-shipment inspection option: Reputable manufacturers welcome third-party inspection. A supplier who resists inspection has something to hide.
3.4 The Decision Guide
Choose a direct factory supplier if: You are ordering container volumes, you need custom sizes or finishes, you want to protect margins by eliminating the distributor markup, and you have the logistics capability to handle imports.
Choose a distributor if: You need small quantities quickly, you lack experience with international trade documentation, or you require local warranty support and installation services.
4. Key Quality Indicators for Wood Look Fiberglass Front Doors Buyers
Experienced buyers focus on specific measurable indicators rather than subjective impressions.
4.1 The Five Critical Measurements
- U-factor: The overall heat transfer coefficient. Lower is better. Look for values below 0.25 for climate zones 4 and colder.
- SHGC (Solar Heat Gain Coefficient): The fraction of solar radiation admitted through the door. Ranges from 0 to 1. Lower values reduce cooling loads.
- Visible Transmittance (VT): The amount of visible light passing through the glazing. Higher is better for natural light.
- Structural Load Rating: The maximum wind pressure the door can withstand. This varies by design pressure (DP) rating, typically DP30 to DP50 for residential applications.
- Air Infiltration Rate: Measured in cubic feet per minute per square foot. Look for values below 0.30 cfm/ft².
4.2 The Cost Breakdown
Understanding the cost structure helps buyers negotiate effectively.
| Cost Component | Percentage of Total Cost |
|---|---|
| Raw materials (resin, fiberglass, foam, glass) | 40-50% |
| Labor and manufacturing overhead | 20-30% |
| Coating and finishing | 10-15% |
| Packaging | 5-8% |
| Logistics and freight | 10-20% |
When a supplier offers a price significantly below the market average, they have likely compromised on one of these components. The most common compromise is the finishing system, which directly affects the wood look realism and durability.
4.3 Total Cost of Ownership
The initial purchase price represents only a fraction of the total cost. Buyers should calculate:
- Maintenance costs: Fiberglass doors require repainting every 10-15 years, versus every 3-5 years for wood.
- Energy costs: A U-factor improvement from 0.35 to 0.20 can save $100-200 per year on heating and cooling for an average home.
- Replacement costs: A quality fiberglass door lasts 30+ years. A wood door may need replacement after 15-20 years.
- Warranty claims: Poor quality doors generate warranty claims that erode distributor margins. A 2% warranty claim rate on a $500,000 annual volume represents $10,000 in lost profit.
5. The Middleman Problem and Direct Sourcing
The traditional distribution chain for entry doors adds significant cost. A manufacturer sells to a distributor at a 20-30% discount from list price. The distributor sells to a dealer at a 10-15% markup. The dealer sells to the contractor at full list price.
For importers and large contractors, this structure makes no sense. A direct factory relationship eliminates two layers of markup.
5.1 The Risk Mitigation Question
Direct sourcing carries risks. The primary concerns are quality consistency, communication, and logistics. These risks are manageable with the right supplier.
- Quality consistency: Mitigated through pre-shipment inspection by a third-party agency.
- Communication: Mitigated by working with suppliers who have dedicated export teams and English-speaking staff.
- Logistics: Mitigated by working with suppliers who provide complete export documentation and coordinate FCL or LCL shipments.
5.2 What a Direct Factory Must Provide
A reliable factory partner provides more than just a low unit price. They should offer:
- Customization: The ability to modify sizes, colors, glass, and hardware to match project specifications.
- Compliance support: Adjusting profile structures and fittings to meet local building codes.
- Documentation: Packing lists, proforma invoices, and full customs documents.
- Production scheduling: Clear lead times based on order volume and customization complexity.
6. Our Manufacturing Capabilities
As a direct factory manufacturer, we operate under the standards described above. This section explains how we meet the requirements that matter to bulk buyers.
6.1 Production Process: From Raw Material to Finished Door
Our production line uses compression molding for the fiberglass skins. The process begins with sheet molding compound, which contains the fiberglass reinforcement, resin, and fillers. The compound is cut to precise dimensions and placed in heated molds that carry the wood grain texture.
The molding cycle takes approximately 4-6 minutes per skin. The molds are heated to around 300°F and subjected to high pressure, which forces the material into the grain details of the mold. After cooling, the skin is trimmed and inspected for surface defects.
The next stage is the assembly line. The fiberglass skins are bonded to a polyurethane foam core that is injected as a liquid and expands to fill the cavity. The foam provides both insulation and structural rigidity. The assembled door blank then moves to the finishing line.
6.2 The Finishing Process
The wood look realism depends on the finishing system. Our process uses a three-coat system:
- Primer coat: Seals the fiberglass surface and provides adhesion for subsequent coats.
- Base color coat: Establishes the primary wood tone, such as oak, mahogany, or walnut.
- Glaze and topcoat: The glaze settles in the embossed grain pores to create depth, followed by a UV-resistant clear topcoat.
The finishing line combines automated spraying with manual inspection. Each door passes through a series of booths where the coating is applied and cured. Between coats, inspectors check for runs, sags, or areas of incomplete coverage.
6.3 Quality Control: Our Multi-Stage Inspection Process
Every door undergoes a series of inspections before packaging. The process goes beyond random sampling.
- Incoming material inspection: Fiberglass compound, foam, and glass are checked against specifications upon receipt.
- In-process inspection: Skins are checked for surface defects after molding. Assembled doors are checked for dimensional accuracy.
- Pre-shipment inspection: Each door is tested for air-tightness and water-tightness. We test 100% of production, not just samples.
- Third-party inspection: We welcome buyer-nominated inspection agencies to verify quality before shipment.
6.4 Certifications and Industry Standards
Our production facility operates under ISO 9001:2015 quality management standards. Our doors are tested to meet the performance requirements of relevant ASTM standards for air infiltration, water penetration, and structural performance.
We provide test reports and certificates with each shipment. For buyers in specific regions, we adjust the profile structure and fittings to match local building codes and energy requirements.
7. Customization and OEM/ODM Options
Bulk buyers often need more than a standard stock door. We support several customization paths.
7.1 OEM Production
OEM (Original Equipment Manufacturer) production means we manufacture doors to your specifications. You provide the design, and we produce it. This is suitable for buyers who have an established product line and need manufacturing capacity.
7.2 ODM Production
ODM (Original Design Manufacturer) production means we provide the design and you brand it. We offer a range of standard wood look fiberglass door models that you can private label. This is suitable for buyers entering the market who need a proven product without the cost of design and tooling.
7.3 Customization Options
Our production line supports full customization on:
- Size: Non-standard heights and widths to match architectural specifications
- Color: Custom stains and paint colors matched to specific samples
- Glass: Low-E, tempered, laminated, and decorative options
- Hardware: Multi-point locking systems, smart locks, and custom hinges
7.4 MOQ and Lead Times
Minimum order quantities depend on the level of customization.
| Order Type | MOQ | Typical Lead Time |
|---|---|---|
| Standard size, standard color | 50 units | 2-3 weeks |
| Custom size, standard color | 100 units | 3-4 weeks |
| Custom size, custom color | 200 units | 4-6 weeks |
| Full OEM with new tooling | Negotiable | 8-12 weeks |
These lead times assume production capacity is available. We provide a confirmed production schedule with each order confirmation.
8. Ordering Process and Logistics
The ordering process for a bulk order follows a structured path.
8.1 The Order Flow
- Inquiry and specification: You provide your requirements, including sizes, finishes, glass packages, and hardware.
- Quotation: We respond with a proforma invoice within 1-2 business days.
- Sample approval: For custom orders, we produce samples for your approval before mass production.
- Production: Your order enters the production schedule. We provide progress updates at key milestones.
- Inspection: You may arrange third-party inspection before shipment.
- Shipping: We handle export documentation and coordinate FCL or LCL shipment.
8.2 Shipping Terms
We support both FCL (Full Container Load) and LCL (Less than Container Load) shipments. For FCL orders, a 40-foot container holds approximately 60-80 doors depending on size. For LCL orders, we consolidate with other shipments to minimize freight costs.
We provide complete export documentation:
- Commercial invoice
- Packing list
- Bill of lading
- Certificate of origin
- Customs declaration documents
8.3 A Case Study: Villa Project in the Middle East
A developer in Dubai ordered 400 wood look fiberglass front doors for a luxury villa community. The project required custom sizes to match architectural drawings, a custom mahogany finish, and multi-point locking systems to meet local security standards.
The order was placed in three shipments over four months. Each shipment contained approximately 130 doors. The first shipment arrived six weeks after order confirmation. All doors passed the buyer’s third-party inspection on the first attempt. The developer has since placed two additional orders for subsequent phases of the project.
9. Why Choose a Direct Factory Partner
The decision to source directly from a factory versus through a distributor depends on your business model and volume.
Choose a direct factory if:
- You order in container volumes
- You need custom sizes or finishes
- You want to protect margins by removing middleman markups
- You have or can develop import logistics capability
Choose a distributor if:
- You need small quantities quickly
- You lack experience with international trade
- You require local warranty service
For buyers who meet the first set of criteria, a direct factory relationship provides a significant competitive advantage.
—
References
[1] U.S. Department of Energy. “Doors and Windows.” Energy.gov. https://www.energy.gov/energysaver/doors-and-windows
[2] ASTM International. “ASTM E283 – Standard Test Method for Determining Rate of Air Leakage Through Exterior Windows, Skylights, Curtain Walls, and Doors Under Specified Pressure Differences.” https://www.astm.org/e0283-19.html
[3] ASTM International. “ASTM E547 – Standard Test Method for Water Penetration of Exterior Windows, Skylights, Doors, and Curtain Walls by Cyclic Static Air Pressure Difference.” https://www.astm.org/e0547-00r16.html
[4] ASTM International. “ASTM E330 – Standard Test Method for Structural Performance of Exterior Windows, Skylights, Doors and Curtain Walls by Uniform Static Air Pressure Difference.” https://www.astm.org/e0330-14.html
[5] National Fenestration Rating Council. “Understanding U-Factor and SHGC.” https://www.nfrc.org/energy-rating-label/
[6] ENERGY STAR. “Windows, Doors, and Skylights.” https://www.energystar.gov/products/windows_doors_skylights
[7] American Architectural Manufacturers Association. “AAMA/WDMA/CSA 101/I.S.2/A440 – Standard Specification for Windows, Doors, and Unit Skylights.” https://www.aamanet.org/
—
We understand that sourcing wood look fiberglass front doors for your projects involves balancing quality, customization, and budget. Our team can discuss your specifications, provide samples, and outline a production schedule that matches your timeline.